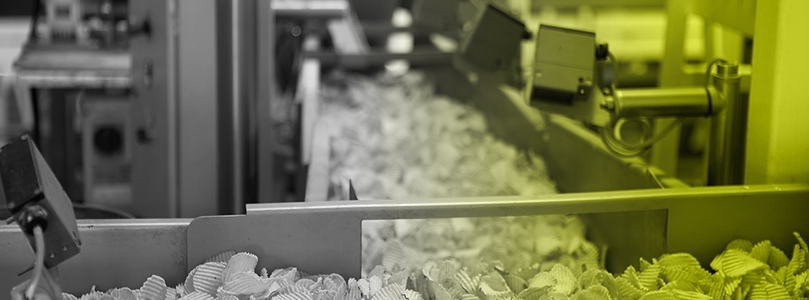
Do you ever get hungry thinking about vision inspection? That’s normal. The food and beverage industry is a pioneer in integrating machine vision into their production lines. As vision inspection tools continue to improve, it has made its way throughout the entire food chain. As a matter of fact, the food industry has forced part of vision’s technological growth as one of the primary equipment buyers.
Key Takeaways:
- Machine vision entered food and beverage production through packaging and traceability before moving onto the line itself.
- Modern systems inspect the product, the container, the label, and the tracking data that leaves with every unit./li>
- Contaminant and foreign material detection now covers defects that are invisible to the human eye, without contact.
How Did Machine Vision First Enter Food and Beverage Production?
As both industries evolve, vision is performing more and more tasks. Packaging inspection was the primary purpose when it was first introduced to the market. Vision was the most efficient way to 100% track and trace the end-product through the supply chain. This is not only to be super organized but is in fact mandated by the FDA for several segments like produce and meat. Should a quality issue arise in a lot, it is vital to address it quickly. This is how producers can reliably keep track of expiry dates and how your grocery store can warn you about that spinach so quickly.
From there, vision spread to the surrounding tasks: UV cure checks to confirm packages are glued correctly, glass container inspection using structured light, and fill level or cap checks using backlighting. 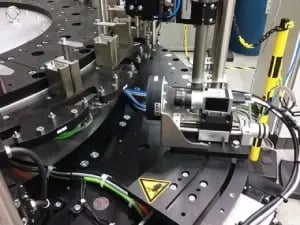
How Does Machine Vision Move from Packaging into the Production Line?
Packaging was how machine vision was first introduced to the industry but has since made its way along the line. Directly in the line, as a matter of fact. Lately, we have all learned the value of high standards pertaining to hygiene. Of course, everyone washes their hands before sitting down to a meal, but how did that meal end up on the plate in the first place?
The equipment producing the food needs to be completely clear of any foreign substances and clean as a whistle. More and more vision systems are being introduced into food and beverage factories to inspect the system manipulating the product. The right perfectly aligned cameras and lighting can easily detect any contaminate, even those invisible to the human eye. This allows any risk to be detected without ever having to be touched by a person.
What are the Applications of Machine Vision in the Food Industry?
Once vision is on the line, its work spans the full path of a product, from the food itself through the container to the data printed on the box.
Foreign Material and Contaminant Detection
Vision systems identify foreign material that infiltrates food and its packaging and flag the affected unit. Spectral cameras can surface contaminants the eye cannot see. The same inspection catches cross-contamination, which is what puts people with allergies at risk.
Product Grading and Sorting
Inspection for color, ripeness, spoilage, and cooking level lets a line hold a consistent standard of quality and appearance before product moves on.
Color and uniformity are harder to judge than they sound. On one meat-packaging line, we built a custom inspection system around a high-speed line-scan camera and LED lighting to read color and uniformity as product ran past. The real value was not only catching the off-color pack, but it was taking that call off a human operator, who gets tired and drifts across a shift. This is in addition to running it 40x faster than manual visual inspection.
Fill Level and Container Integrity
Vision systems verify fill levels, confirm that bottles and jars are intact, and check that caps and closures are sealed correctly. A single X-ray pass can bundle several of these at once, adding mass measurement and seal integrity simultaneously.
 Distinguishing a real defect from normal material can be a problem though. When developing a line inspecting single-serve coffee cups from pre-laminated aluminum, the cups left the press twelve at a time and ran the guide rails at 1 to 8 m/s. The catch was that genuine defects looked almost identical to the natural stretch marks that aluminum picks up as it is formed. Separating the two took very specific reference data and carefully written vision scripts before t
he system could tell a good cup from a bad one consistently. Once that was solved, conforming cups were stacked for the next stage while defective ones were diverted to recycling, at roughly 1,800 cups per minute per station and about 30 inspections every second. Impressive, right? That’s why we love vision inspection at Averna Powered by Spherea.
Presence Verification and Missing Component Detection
Vision confirms that every expected element is present before it advances, so nothing ships incomplete.
Packaging Inspection
Misprinted or illegible packaging is caught before it leaves the line. Systems notice when the wrong product or destination label is substituted, and when lids do not match the rest of the pack. Vision also verifies that recycled packaging materials are clean and in good repair. This is where several early food applications still live, such as UV cure checks on packages to ensure it's glued correctly and glass container inspection using structured light.
Label Inspection and Verification
Mislabeled food can trigger an allergic reaction and a government-mandated recall. The numbers make this the highest-stakes role on the line. Undeclared allergens such as milk, peanuts, or wheat accounted for 39 percent of all U.S. food recalls in 2025, and undeclared allergens have been the leading cause of recalls in nearly every quarter for years. The failure starts when an updated recipe spec never reaches a label artwork created months earlier. Vision removes products mislabeled through machine or human error, and flags misaligned or wrinkled labels.
Track and Trace and Ingredient Traceability
Systems read and match product codes, dates, lots, and barcodes so nothing leaves the line with incorrect data. They stop illegible or missing codes and compile a tracking history for each package, ready for a future recall or audit.
The FDA Food Traceability Rule, known as FSMA 204, requires enhanced records for foods on the Food Traceability List, including traceability lot codes and key data elements captured at defined tracking events, produced to the FDA within 24 hours of a request. The compliance date moved from January 20, 2026 to July 20, 2028, and in November 2025 congress directed the FDA not to enforce the rule before that date. The requirements themselves are unchanged.
Where Does AI Fit In?
Regular vision systems follow rules, and they follow them well. The problem is that food does not follow rules. Two good tomatoes never look quite the same, and a rule that is strict enough to catch the bad ones will start throwing out the good ones too. This is where AI comes into vision inspection. It learns what an actual defect looks like versus a good unit, and it gets better the more product it sees. But this cannot replace people. AI can copy a lot of what an operator does, it just cannot match the instinct of someone who has done the job for years. The best lines use both!
Why Does Vision Inspection Protect Both Consumers and Brands?
The consequences of skimping on equipment inspection are astronomical, both for the foodie and the company. Dirty equipment is bad enough on its own, but allergens raise the stakes to potentially cause real harm. This business needs to look out for their customer and for their brand. Nobody wants to eat what will hurt them. Except maybe French Fries.
At the end of the day, vision inspection plays a huge role in looking out for the companies that manufacture food products and those that eat food. That does not exclude a whole lot of people.
Bringing Vision Inspection to Your Line
No two food lines look alike, so no single system fits them all. The work is in the integration: matching the cameras, optics, the lighting, and the inspection logic to your product and the defects that actually matter to you.
That is what Averna designs and builds. To see what that could look like on your own line, talk to our vision experts.
Still hungry?
Find out how we supported ViskoTeepak through their transition to vision inspection.
Get in touch with our experts or navigate through our resource center.


