
If a part is going into a plane or a defense platform, nobody simply trusts its reliability. A dense set of program-specific requirements are created and a significant amount of testing standards offers peace of mind. Somewhere in there, you start to suspect that the only thing tested more thoroughly than the aircraft is the paperwork that it comes with.
And it makes sense, since there are few industries that carry higher consequences for failure. How do these testing standards ensure safety?
Key takeaways:
- Standards, regulations, and OEM requirements are separate layers. A standard such as DO-160 defines a test, a regulator such as the FAA or EASA decides what certification demands, and aircraft manufacturers add their own specifications above and beyond
- The same component answers to different standards at different stages: design verification, environmental qualification, production test, and MRO.
- Meeting a standard is a claim you have to prove again and again, unit after unit. That makes it a test-engineering challenge as much as a documentation one.
What are Aerospace Testing Standards?
An aerospace testing standard is a documented, repeatable test procedure that defines how a component is evaluated and what result it must reach to pass. Its job is consistency. A part tested to DO-160 in one lab should get the same verdict in another, whatever supplier or program it belongs to.
Standards come from independent bodies. Civil avionics standards are published by RTCA and EUROCAE; the military MIL-STD series is owned by the US Department of Defense. None of these bodies can approve your product.
The naming indicates the origin. The DO series, with its European ED equivalents, comes from RTCA and EUROCAE for civil airborne equipment.
The MIL-STD series comes from the US Department of Defense for military use. Many programs apply both, since a military aircraft still carries commercial-derived avionics.
Regulations are what an authority requires, and approval comes from there. The FAA and EASA reference the relevant standards through instruments like the Technical Standard Order, TSO in the US and ETSO in Europe. Meeting the standard is necessary but not sufficient. A TSO authorization lets you manufacture the part, but installing it on a given aircraft still means proving it meets that aircraft's own certification basis.
Aircraft and platform makers then add their own specifications on top, usually stricter than the baseline. A unit can pass DO-160 and still fail an OEM's acceptance criteria.
How the Standards Apply Across the Test Lifecycle
A single component does not face all of these standards at once. It meets different ones at different points in its life, and the type of testing shifts as it goes. The design assurance work that matters before first flight has little in common with the functional checks a repair shop runs on the same unit years later.
Across a program, this lines up with the verification and validation (V&V) effort, each standard supplying the test evidence a given step depends on. Four stages cover most of it.
| Stage | What you are proving | Representative standards |
|---|---|---|
| Design verification | The hardware and software are correct by design | DO-254 (electronic hardware), DO-178C (software), with ARP4754A and ARP4761 governing system development and safety above them |
| Environmental qualification | A unit survives its real operating environment | MIL-STD-810 (military), DO-160 (avionics environmental and EMC), MIL-STD-461 (military EMC) |
| Production test | Every unit built matches the qualified design | Functional and acceptance testing against the unit's performance and interface specs, which reference standards such as MIL-STD-704 (electrical power) and MIL-STD-1553 or ARINC 429 (data buses) |
| In-service and MRO | A repaired or overhauled unit still conforms before it returns to service | Functional test on the line-replaceable unit against the same interface and performance criteria |
Qualification happens once per design. Production and MRO testing repeats for the life of the program, unit after unit, which is why it tends to drive the investment in aerospace and defense test equipment.
The Core Defense and Aerospace Testing Standards, by Category
These testing standards sort into four groups:
Environmental and Durability
This group asks whether the component survives its physical operating conditions through environmental testing: temperature, vibration, shock, altitude, humidity, and the rest of what a real deployment throws at it.
- MIL-STD-810 covers military equipment on any platform, from a handheld radio to a vehicle-mounted system. Its current revision, MIL-STD-810H, defines more than two dozen tailorable laboratory test methods, from temperature, humidity, and altitude to vibration, shock, and salt fog, applied through a tailoring process rather than as a fixed pass or fail list. Originally created by the U.S. Department of Defense, it serves as a de facto reference for rugged and military equipment internationally.
- DO-160 is written around aircraft, and it is the environmental reference civil authorities recognize for airborne equipment. The current DO-160G organizes testing into 26 sections, covering environmental categories such as temperature, altitude, vibration, humidity, and fluid susceptibility, alongside power input and electromagnetic conditions. Jointly published by RTCA (U.S.) and EUROCAE (Europe as ED-14), it is the international reference for civil airborne equipment and is often invoked on military programs that use commercial-derived avionics.
The two overlap conditions like vibration and humidity, but each carries methods the other does not.
Electromagnetic Compatibility and E3
Here the question is how a system behaves in a crowded electromagnetic environment: what it emits, and what it tolerates without malfunctioning.
MIL-STD-461 is the military EMC standard and the de facto reference for defense programs worldwide. The current MIL-STD-461G groups its requirements into conducted and radiated emissions and susceptibility, each with numbered test methods such as CE102, RE102, CS101, and RS103. Created as a U.S. military specification, it is widely adopted by international defense forces to govern electromagnetic interference.
DO-160 carries the equivalent EMC sections for civil avionics. Its electromagnetic sections (Sections 15 through 23, plus Section 25) are recognized by worldwide aviation agencies including the FAA and EASA.
Both sit inside the wider field of electromagnetic environmental effects, or E3, which also takes in high-intensity radiated fields and lightning.
Hardware and Software Design Assurance
DO-254 and DO-178C work differently from the rest. They govern how electronic hardware and software are developed and verified, with the required rigor scaled to the consequences of failure through Design Assurance Levels, from DAL A for functions whose failure is catastrophic down to DAL E. DO-254 governs the lifecycle of complex electronic hardware such as FPGAs and ASICs, DO-178C the software lifecycle.
At the top level, DO-178C expects coverage as demanding as modified condition/decision coverage. Developed jointly by RTCA and EUROCAE (as ED-12C for software and ED-80 for complex hardware), both standards form the international baseline for airborne system certification.
ARP4754A and ARP4761 sit above both, tying each item back to the aircraft-level safety assessment. Originally developed by SAE International in the U.S., these system-level guidelines are now widely recognized by civil aviation authorities as an accepted means of compliance for system development and safety.
These standards also govern the newest aircraft. Electric vertical-takeoff (eVTOL) aircraft are certified against DO-178C, DO-254, and DO-160 under dedicated frameworks such as EASA's SC-VTOL, often at the most demanding assurance levels.
How Conformance Is Verified in Production and MRO
Meeting a standard once, on one qualification unit, is a milestone. Meeting it on every unit built, and again after every repair, is the larger and longer job, and it absorbs most of the test effort across a program's life.
Functional Test and Automated Test Equipment
In production, each unit goes through a functional acceptance test: power the unit up, exercise its interfaces, and confirm the outputs match spec.
To test avionics line-replaceable units (LRU) that includes:
- Driving and monitoring its data buses, such as ARINC 429 or MIL-STD-1553
- Feeding it electrical power that matches the MIL-STD-704 profile
- Reading back its signal and RF outputs to check they land inside the limits
Running that by hand at volume does not work, so manufacturers use automated test equipment, a set of instruments under software control that executes the same sequence identically on every unit and records the result. The payoff is repeatability and traceability, which is what a certification authority or a customer audit wants to see.
Repeatability from Production to MRO
A unit is tested at more than one point in its life, ideally against a consistent definition of pass. An LRU qualified during development is tested again on the production line, then repeatedly through its service life each time it is removed, repaired, and returned to service.
MRO test benches confirm a repaired unit still meets its original acceptance criteria before it goes back on an aircraft. Generic, modular benches carry their weight here, since one bench that can test many LRU types costs far less to own and support than a dedicated rig for each.
Proven Conformance in Testing with Averna
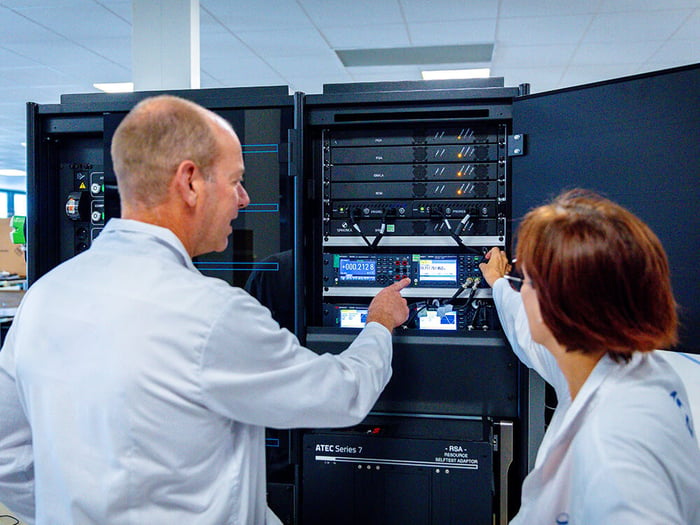
Averna Powered by Spherea offers test solutions for defense and aerospace manufacturers and MROs: environmental and EMC test environments aligned with MIL-STD-461, MIL-STD-810, and DO-160, and modular ATEC benches for line-replaceable unit production and maintenance. Avionics testing, radars, batteries, actuation systems, you name it, and we will bring your test systems to the next level.
You may also be interested in…

Find out more about our capabilities in the industry with our aerospace expertise brochure.


