
Much like other engineering disciplines, test engineering focuses on in-depth analysis and methodical processes that produce high-quality results. Where civil engineers design, build and maintain infrastructure like bridges or dams, test engineers design, develop and maintain integrated systems that test, measure and inspect all the features and functionality of a high-tech product at any and every stage of the product’s lifecycle, both to ensure it meets designated specifications as well as attains maximum quality, safety and efficiency levels.
While there are many reasons why test engineering is a necessary and crucial part of preparing a product for market, here are seven of the most important reasons why:
1. Harmonizing the entire product lifecycle
Typically, a product lifecycle includes several stages, including product design, design validation, new product introduction (NPI), manufacturing, and repair and return screening. So often, test engineers like those at Averna, work closely with original equipment manufacturers (OEMs) to develop validation routines and test systems required for each phase. Beginning with the first phase, product design, their focus is usually on automation and an intelligent, integrated flow from one stage to the next.
2. Design For Testing streamlines development
As high-tech products become more complex and OEMs face increasing competition, test engineers have shown that a design for testability (also known as “design for testing” or DFT) stage adds enormous value to product development processes. For example, Averna’s test engineers will typically collaborate with product designers to integrate certain feature functionality like smart chips, measurement capabilities, and diagnostic routines into their product designs. These elements make it easy to run automated tests on all functionality, generate valuable data for analysis and troubleshooting, and speed up the product development cycle.
3. Design For Manufacturing simplifies production
When designing a product testing approach and a plan, another area where test engineering adds a great deal of value is through design for manufacturability (also known as “design for manufacturing” or DFM). Integrating DFM principles allow significant time, material and resource savings during the production stages. Averna’s test engineers are not only concerned with complete test coverage, but also with product quality and testing efficiency. As such, they typically assist OEMs with integrating DFM principles into their product designs so that when a new product reaches the manufacturing stage, there are no costly delays or surprises because every aspect of the product has been considered in terms of how the final product will be assembled and tested. This greatly streamlines the product lifecycle and is typically the reason for significant time, material, and resource savings during the production stages, further underlining the value that test engineering can bring to high-tech product development.
4. Test automation speeds-up time to market while lowering costs
Product testing has become increasingly complex due to the convergence of many different technologies into single products like smartphones, wearable devices, automotive infotainment systems, and medical devices. In addition to the obvious challenge of testing a greater amount of technology in increasingly smaller devices, there is also the fact that product competition is strong while shelf life is shorter and shorter. Many of today’s electronics manufacturers are therefore optimizing their test architecture and test routines to cover more product functionality as quickly as possible. By using standardized test software such as LabVIEW and NI TestStand, they can implement batch and parallel testing to speed throughput, optimize instrument use, automate standard operating procedures (SOPs), and easily gather test result data to further improve processes. It’s clear that today’s complex in-vehicle systems require new test approaches.
5. Automated test stations accelerate throughput and improve quality
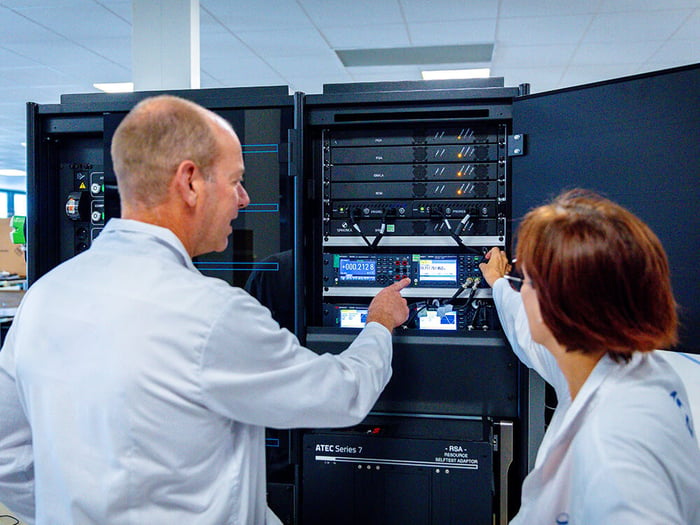
An important component in thorough product testing is automated test equipment (ATE) – assembly test stations, functional test stations, and ESS test stations – that is used to verify assembled components such as semiconductor chips and boards, or to functionally test partially or fully assembled units. Additionally, depending on how and where the product is used, there may be specialized test stations, fixtures, and chambers used for testing small unit samples to ensure that they operate when vibrated, dropped, immersed, or exposed to electromagnetic or extreme temperatures, and so on. Units that fail at any stage are typically routed to repair stations for troubleshooting and reconditioning.
6. Vision inspection systems quickly identify defective products
Over the past few years, advancements in vision technologies, cameras, lasers, optics/lighting, and machine-learning capabilities have been a boon for manufacturers dedicated to improved product quality. Consequently, many of these manufacturers have integrated advanced vision inspection and machine vision systems into their production lines in order to verify correct product assembly and ensure zero defects. For example, in the automotive sector, Tier 1 and 2 suppliers ensure that products such as custom-built vehicle dashboards and cockpits are perfectly matched to OEM specifications and sales orders, guaranteeing that suppliers respect service level agreements (SLAs) and avoid penalties from OEMs.
Vision inspection and machine vision systems are, in effect, highly intelligent quality-assurance (QA) systems that can, with high precision, scan large numbers of both electronic and non-electronic products (e.g., pills, processed foods) simultaneously to detect flaws, as well as measure, classify and sort these products. These systems can also store comprehensive test results, ensuring that all product details are captured and accessible for analysis and traceability.
7. Fast test station replication helps OEMs reach their markets
If the product being tested is bound for the consumer electronics or automotive markets, there’s a good chance that multiple high-volume test stations, often including robotics and automated assembly lines, will be needed to satisfy consumer demand. Additionally, identical test stations may be required in multiple countries to ensure simultaneous worldwide product releases. Another driver for global test station deployment is cost. Many OEMs have chosen contract manufacturers (CMs) and electronics manufacturing services (EMS) in lower-cost countries for their manufacturing operations. The logistics needed to ensure synchronized production around the world are significant and usually require the support of a test engineering company with build-to-print expertise that can rapidly source and assemble identical test stations, and then ship and integrate them into CM and EMS sites around the world.


